Engineering Global Skylines Through Precision Metallurgy
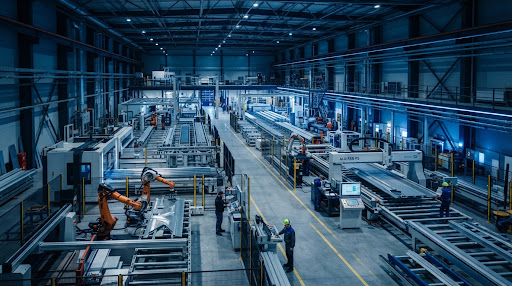
State-of-the-Art 150,000 m² Automated Manufacturing Hub & Facade Engineering Excellence. Supplying monument-scale architectural envelopes to over 60 international sovereign territories.
Spanning 4 robotic fabrication halls
German 5-axis ±0.3mm tolerance
Hyperbolic, honeycomb, acoustic
EU, MENA, Americas, APAC
PPG / AkzoNobel PVDF Class 1
Two Decades of Monumental Cladding & Structural Realization
Founded with the foundational mission to close the gap between daring parametric architectural concepts and industrial-scale manufacturability, ALUMAX has grown from an artisan metallurgical workshop into one of the world's most capable envelope fabrication partners. Over 20+ years, our facade engineering studio has collaborated directly with benchmark global architectural practices—including Foster + Partners, Zaha Hadid Architects, and Skidmore, Owings & Merrill (SOM)—turning complex fluid hyperboloids, extreme wind-shear canopies, and blast-resistant assemblies into pristine, install-ready reality.
Two Decades of Innovation & Global Expansion
Chronological milestones tracking ALUMAX's progression from precision artisan workshops to global benchmark façade engineering.
Pioneering Solid Cladding
Commissioning of the first automated 3.0mm solid PVDF coil lines. Initial export deliveries for high-traffic civil infrastructure including terminal concourses at Hong Kong International Airport.
Honeycomb & 3D Hyperbolics
Strategic expansion into the unified 150,000 m² campus. Attainment of European CE & EN 13501-1 A2 non-combustible composite core certification and specialized roll-curving capabilities.
Digital BIM & Smart Facades
End-to-end integration of motorized solar shading systems, parametric CAD-to-CNC LOD 400 fabrication pipelines, and international logistics directly servicing global supertall towers.
Advanced Tooling & Machinery Matrix
Engineered to eliminate project bottlenecks on monument-scale envelopes. Deploying precision multi-axis CNCs, robotic laser workstations, and automated continuous coating tunnels built to ASTM & EN tolerances.
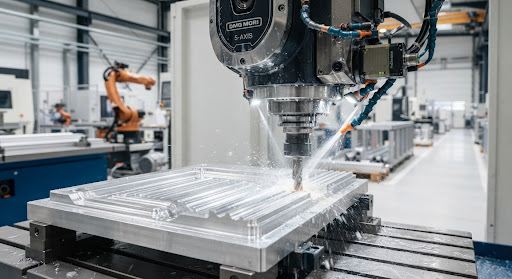
5-Axis CNC Precision Centers & Roll-Bending
Engineered for double-curved hyperbolic panels, compound faceted louvers, and slotted cassette perimeters. Driven directly by parametric BIM LOD 400 CAM pipelines with real-time tool compensation.
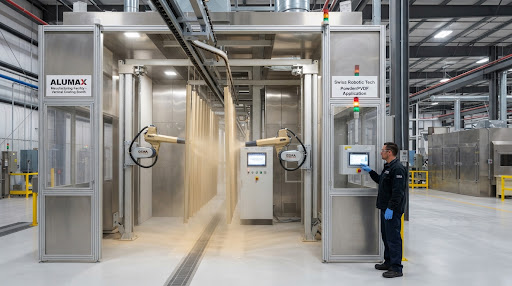
Automated PVDF & Powder Coating Lines
Class 10,000 pressurized cleanroom spray cabins with 14-stage zirconium pre-treatment. Certified by PPG Duranar, AkzoNobel Interpon D3000, and Valspar for 20-30 year maritime architectural warranties.
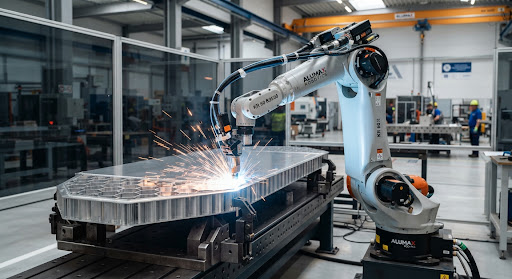
Robotic Laser Welding & Core Bonding Cells
Dual-fiber 12kW automated robotic welding cells with seam-tracking sensors. Eliminates cosmetic heat deformation on front-facing architectural surfaces while providing complete structural alloy continuity.
Rigorous End-to-End Quality Protocol
Eliminating on-site installation risks through a certified 4-phase testing regimen. From raw molten ingot spectroscopy to hurricane chamber mock-ups and serialized crate tagging.
Raw Metallurgy & Substrate Purity
Optical emission spectroscopy verifies 3003-H14 / 5052-H32 alloy chemical purity before slitting. Ultrasonic continuous caliper scans monitor coil gauge across full coil widths.
3D Cloud Geometry & CNC Tolerances
High-speed Leica laser coordinate scanners map fabricated 3D curved surfaces and slotting hole positions directly against Navisworks & Revit BIM IFC coordinate models.
Severe Climate & CWCT Stress Testing
In-house dynamic testing chambers subject 1:1 scale facade cassettes to 3,600 Pa cyclic wind loads, deluge water penetration tests, and 4,000-hour ASTM B117 salt fog corrosion exposure.
Crate Serialization & Digital Dossier
Every panel is laser-etched with a unique QR / RFID code linking to raw coil mill certificates, coating batch logs, QA engineer digital stamps, and installation grid coordinates.